Internal Ring Gear Manufacturing and Inspection for Planetary Drives
A practical engineering guide to internal tooth generation, heat-treatment distortion and datum-based inspection, with RFQ, inspection and application details that can be used when evaluating a new or replacement planetary transmission.
Engineers usually select planetary gearing for torque density and packaging, yet the reliability of the stage depends on the less visible relationships among tooth geometry, datums, bearings and operating duty. This guide focuses on internal tooth generation, heat-treatment distortion and datum-based inspection. It is written to help a buyer, design engineer or maintenance team define the problem in measurable terms before comparing suppliers. The goal is not to turn every application into the same catalogue selection, but to show which evidence changes the technical decision and which assumptions should remain open until the actual drawing or duty data is available.
Негізгі тақырып - internal ring gear manufacturing. In practice, it touches internal gear shaping, heat-treatment ovality, root clearance, and usually at least one of ring-wall stiffness, pitch runout or housing fit. These factors are linked. A correction to one item can improve one failure mode while worsening another, which is why planetary gearing should be reviewed as a stage rather than as a single isolated tooth count.
Нағыз күш жолынан бастаңыз
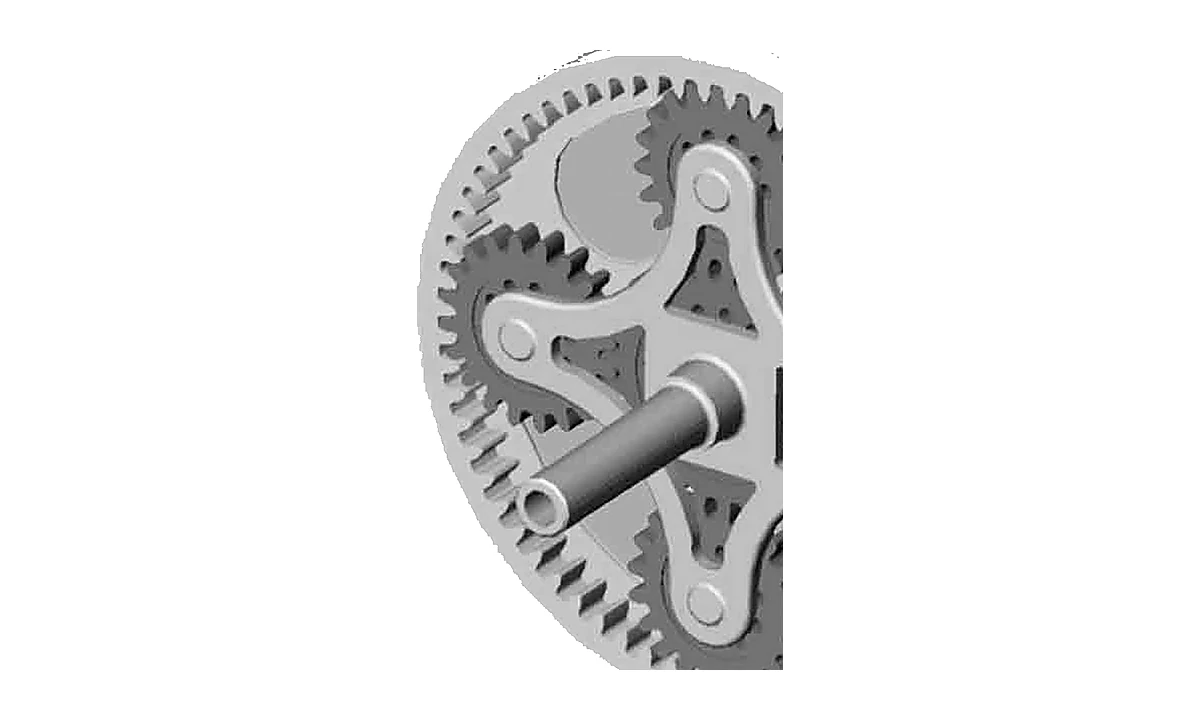
A conventional planetary stage contains a central sun gear, multiple planet gears, an internal ring gear and a carrier. Torque is split across the planet branches and recombined through the carrier or another active member. That architecture makes the transmission compact, but it also means the stage reacts through several structural paths at once. When reviewing internal ring gear manufacturing, first identify the driven member, the held member and the output member. Without that configuration, a ratio or torque statement can be misleading because the same tooth counts can produce different kinematic behavior under a different fixed-member arrangement.
For internal tooth generation, heat-treatment distortion and datum-based inspection, the load path should be traced from the input interface through every mesh and bearing support to the output and housing reaction. Record where internal gear shaping enters the problem and how heat-treatment ovality changes under continuous torque, peak torque, reversal or coast-down. This makes it easier to decide whether the limiting issue is tooth stress, bearing reaction, carrier stiffness, spline fit, lubrication, thermal behavior or a combination of these. It also prevents the common procurement error of solving a visible tooth defect while leaving its root cause in the assembly.
Ұқсас планеталық беріліс құралын қарау
Маңызды өлшемдер
Useful specifications connect a requirement to a method of verification. For this topic, that means turning phrases such as “high precision,” “heavy duty,” or “low noise” into drawing features, operating values and inspection evidence. Depending on the project, the important controls may include internal gear shaping, heat-treatment ovality, root clearance, ring-wall stiffness. The chosen controls should be tied to the functional datums of the assembly. A gear-quality value measured from an arbitrary surface is less useful than a slightly broader inspection plan referenced to the bore, spline, pin circle or other datum that actually locates the gear in service.
When an old sample is the only evidence, separate original geometry from wear. Polished flanks, pitting, plastic deformation, fretted bores and damaged spline teeth can move measurements away from the intended design. Whenever possible, compare several teeth, both faces, multiple mating members and unworn reference surfaces. For internal ring gear manufacturing, photographs of the contact pattern and the assembly orientation can be as important as a single dimensional report because they show whether the problem is distributed or localized.
| Тексеру | Тұтқындауға болатын дәлелдемелер | Инженерлік себеп |
|---|---|---|
| Internal Gear Shaping | Capture the drawing requirement, measured condition or operating evidence for internal gear shaping. | It can change the acceptance decision for internal ring gear manufacturing and inspection for planetary drives. |
| Heat-Treatment Ovality | Capture the drawing requirement, measured condition or operating evidence for heat-treatment ovality. | It can change the acceptance decision for internal ring gear manufacturing and inspection for planetary drives. |
| Root Clearance | Capture the drawing requirement, measured condition or operating evidence for root clearance. | It can change the acceptance decision for internal ring gear manufacturing and inspection for planetary drives. |
| Ring-Wall Stiffness | Capture the drawing requirement, measured condition or operating evidence for ring-wall stiffness. | It can change the acceptance decision for internal ring gear manufacturing and inspection for planetary drives. |
| Pitch Runout | Capture the drawing requirement, measured condition or operating evidence for pitch runout. | It can change the acceptance decision for internal ring gear manufacturing and inspection for planetary drives. |
Өндірістік вариация қалай кезеңге енеді
Planetary transmissions combine several tolerances in one compact assembly. A small change in internal gear shaping may interact with root clearance, while ring-wall stiffness can shift the contact toward one side of the face width. Manufacturing planning therefore needs a datum chain, a heat-treatment strategy and a final inspection route that are consistent with how the part functions. Hard finishing should not be specified automatically; it is used when the material, hardness, gear quality and economics justify it. The same principle applies to grinding, honing, lapping, shaping and other processes.
Set-level consistency is especially important when multiple planet gears share load. If planets come from different revisions or manufacturing states, the assembly can acquire unequal backlash or load distribution even when each part appears individually acceptable. For internal tooth generation, heat-treatment distortion and datum-based inspection, lot control and identification can therefore be part of the technical solution. This is one reason a matched set is often the lower-risk purchase when the original stage is badly worn or its maintenance history is uncertain.
Өтініш беру шарттары Жауапты өзгертеді
A solution that works in a steady industrial reducer may be unsuitable for a servo axis, crawler final drive, wheel hub or slewing system. Servo duty emphasizes reversing behavior, stiffness and positioning. Mobile equipment adds shock, sealing and field contamination. Slewing duty can combine high ratios with intermittent peaks and brake reactions. Continuous industrial drives make thermal capacity and oil condition more visible. The design review for internal ring gear manufacturing should therefore name the machine, not just the gearbox.
Кіріс жылдамдығының диапазонын, үздіксіз шығыс моментін, шың немесе іске қосу моментін, сағатына іске қосылуын, кері жиілігін, жұмыс циклін, қоршаған орта температурасын, орнату орнын, майлау материалын, күтілетін қызмет мерзімін, радиалды және осьтік жүктемелерді және кез келген сыртқы тежегіш немесе қозғалтқыш интерфейсін көрсетіңіз. Бұл мәндер әлі белгісіз болса, оларды визуалды түрде ұқсас өнімнен алынған мәнмен алмастырудың орнына ашық элементтер ретінде белгілеңіз. Бұл бағаны бақылауға мүмкіндік береді және машина тобы кейінірек нақты жұмыс деректерін ұсынған кезде қайта өңдеуді азайтады.
Планетарлық беріліс жинағының опцияларын салыстырыңыз
Сәтсіздіктерді талдау кезінде не іздеу керек
Failure evidence should be collected before parts are cleaned aggressively or discarded. For internal tooth generation, heat-treatment distortion and datum-based inspection, look for asymmetric contact, localized pitting, scuffing, root cracks, debris indentation, fretting at interfaces, discoloration, bearing damage and looseness at pins or splines. The location of the damage relative to load direction can help separate overload from misalignment or lubrication problems. Oil samples, filter debris and vibration trends add context when they are available.
Сынған беріліс әрқашан бастапқы ақаулық бола бермейді. Қаттылығын жоғалтатын мойынтірек торды жылжытуы мүмкін; тасымалдаушы түйреуіш тозуы және планетаның орнын өзгертуі мүмкін; корпус болт жүктемесі кезінде деформациялануы мүмкін; немесе май беру жолы бір торды аш қалдыруы мүмкін. Сондықтан тексеру көрінетін зақымдалған элементтен тысқары болуы керек. Егер беріліс себебін түзетпей ауыстырылса, жаңа бөлшек тезірек істен шығуы мүмкін, себебі оның тозбаған геометриясы бастапқыда зақымдалған түйіспелі компоненттің кішірек аймағына жүктеме түсіреді.
Осы тақырып бойынша жеткізушінің RFQ тексеру тізімі
- Геометрия: drawing or verified values for tooth counts, module/DP, pressure angle, tooth form and the interfaces relevant to internal gear shaping.
- Дәлдік: drawing tolerance, gear-quality requirement and the measurement datum needed to evaluate heat-treatment ovality.
- Материалдық бағыт: көрсетілген материал және термиялық өңдеу, оның ішінде конструкциямен басқарылатын кездегі қаттылық немесе корпус талаптары.
- Міндет: үздіксіз және шыңдық момент, кіріс жылдамдығы, кері айналдыру, сағатына іске қосу, жұмыс циклі, температура және майлау.
- Жұптасу дәлелдері: күн, планеталар, сақина және тасымалдаушы деректері, әсіресе тек бір ғана істен шыққан бөлік сатып алынған кезде, бір торға әсер етеді.
- Саны және бақылау мүмкіндігі: прототип, қызмет көрсету партиясы немесе өндіріс көлемі, сызбаны қайта қарау және қажетті тексеру жазбалары.
Пайдалы қосымша қоғамдық сілтеме - бұл planetary transmission system resourceОны ағымдағы жобаның сызбасы мен тапсырма деректерінің орнына фондық контекст ретінде пайдаланыңыз.
Қайта өңдеуден аулақ болатын шешім қабылдау жолы
First, define the failure, performance target or replacement need. Second, establish authoritative geometry from drawings, samples and mating parts. Third, connect the required duty to the load path and identify which controls are actually critical for internal ring gear manufacturing. Fourth, define manufacturing and inspection around the functional datums. Fifth, review the complete mating set and assembly before final release. This sequence is slower than guessing from a photo, but it is faster than repeating machining after a mismatch is found during assembly.
Жаңа конструкциялар үшін дәл осындай тәртіп шамадан тыс сипаттамалардың алдын алуға көмектеседі. Беріліс сапасының өте тығыздығы, агрессивті термиялық өңдеу талабы немесе күрделі әрлеу жолы, егер корпус, мойынтіректер немесе тасымалдаушы бірдей дәлдікті қолдамаса, машинаның жұмысын жақсартпай, құнын арттыруы мүмкін. Керісінше, жүктемені бөлуді немесе шығыс позициясын басқарған кезде кішігірім төзімділік маңызды болуы мүмкін. Инженерлік мақсат - әрбір өлшемді бірдей тығыз ету емес, дәлдікті кезеңнің мінез-құлқын өзгертетін жерге қою.
Суреттеріңізді шолуға жіберіңіз
Тапсырысты шығармас бұрын жауап берілетін сұрақтар
- Which member is input, which is fixed, and which is output in the stage related to internal ring gear manufacturing?
- Which drawing or sample defines internal gear shaping, and is that evidence from the current revision?
- How will heat-treatment ovality be verified at incoming inspection or final assembly?
- Does the duty include shock, reversal, braking or temperature conditions that change the acceptance of root clearance?
- Тісті берілістер, тасымалдаушы, мойынтіректер және интерфейстер әлі де жұмыс істей ме, әлде ауыстыру аймағына сәйкес келетін жиынтық кіруі керек пе?
- Қабылдаушы топ жеке басын және маңызды сипаттамаларын растай алуы үшін жөнелтіліммен бірге қандай тексеру жазбасы болуы керек?
Өндірістік шолуды сұрау
EVER POWER планеталық беріліс сызбаларын, үлгілерін және пайдалану туралы ақпаратты өндірістің орындылығы мен бағасын анықтау үшін қарап шыға алады. Қолжетімді файлдарды, санын, тағайындалған жерін және жұмыс туралы ақпаратты келесі мекенжайға жіберіңіз: [email protected]Егер жоба ауыстыру болса, бөлшектемес бұрын фотосуреттерді қосыңыз және күннің, планеталардың, сақинаның, тасымалдаушының және мойынтіректердің тексеруге қолжетімді екеніне назар аударыңыз. Жетіспейтін мәндер үнсіз бағалаудың орнына растау үшін анықталады.